 SOFT
Quality is built into a production chain, not inspected in at the end. This is a walkthrough of the four gates every SOFT LIGHT order passes — what gets measured at each, with real AQL arithmetic — and the golden-sample discipline that keeps your third order identical to your first.
- What does a lighting factory's QC actually cover?
- Why the in-house chain matters
- Four inspection gates
- What we actually measure at IQC
- Inside the SMT line: process control, not luck
- Aging, safety and the tests behind 'it works'
- AQL sampling in plain numbers
- Golden sample discipline
- Third-party inspection: how we cooperate
- What to take from this
What does a lighting factory's QC actually cover?
Short answer: four inspection gates — incoming materials, in-process, final and pre-shipment — plus the sample discipline that connects them. Certificates tell you a system exists; the gates tell you whether it bites. This post walks through each gate as it operates on our lines in Zhuhai and Huizhou, including the checks we run that never appear on a datasheet.
Why publish this? Because buyers who understand the process audit faster, write better specifications and have fewer disputes. A buyer who knows what IQC can and cannot catch, for instance, stops asking it to catch design errors that were locked in months earlier.
Why the in-house chain matters
Most lighting brands assemble from bought-in parts and never see their suppliers' suppliers. When a coating fails or an LED bin drifts, responsibility gets argued across three companies. Because our group handles tooling, metal forming, laser welding, spraying, SMT electronics and final assembly in-house, a problem is traced to its source the same day — the spray line foreman and the QC manager work fifty metres apart, not on opposite sides of a purchase order.
The practical benefit shows up in repeat orders. Colour consistency across production runs is a bin-control problem at LED purchasing plus a process-control problem at SMT; both sit inside our walls. That is why we can commit to 3-step SDCM binning in writing for project orders — the colour consistency guide explains what that commitment means on the ceiling.
Four inspection gates
Every order passes four gates. Failures stop the line — they do not get shipped with an apology.
| Gate | Where | What is checked | If it fails |
|---|---|---|---|
| Incoming (IQC) | Materials warehouse | LED bins, drivers, housing castings, diffusers against purchase spec | Lot rejected and returned to supplier |
| In-process (IPQC) | SMT, spraying, assembly lines | Solder joints, spray thickness, assembly torque — sampled per shift | Line held; deviation corrected before restart |
| Final (FQC) | End of assembly | Full function, aging, high-potential and visual checks per AQL plan | Unit repaired or scrapped; batch re-audited |
| Pre-shipment (FQC-2) | Packing area | Carton condition, labels, accessories against packing list | Packing redone before container loading |
What we actually measure at IQC
Incoming inspection is where cheap components get caught, so it is where we spend sampling effort. LED reels are checked against the binning spec — colour point, forward voltage — because a mis-shipped bin discovered at assembly costs a line stop, discovered by the customer costs a reputation. Drivers are sampled functionally and cross-checked against the golden sample's behaviour. Castings and housings get coating-thickness and dimensional checks; diffusers get material verification, since a substituted diffuser changes both light distribution and UV life.
The discipline that makes IQC work is traceability: every accepted lot carries a lot number that follows it to finished goods. When a field question arrives months later — as one eventually will — we can trace the unit back to its LED reel and driver lot within an hour. Buyers rarely ask about traceability until the day they need it.
Inside the SMT line: process control, not luck
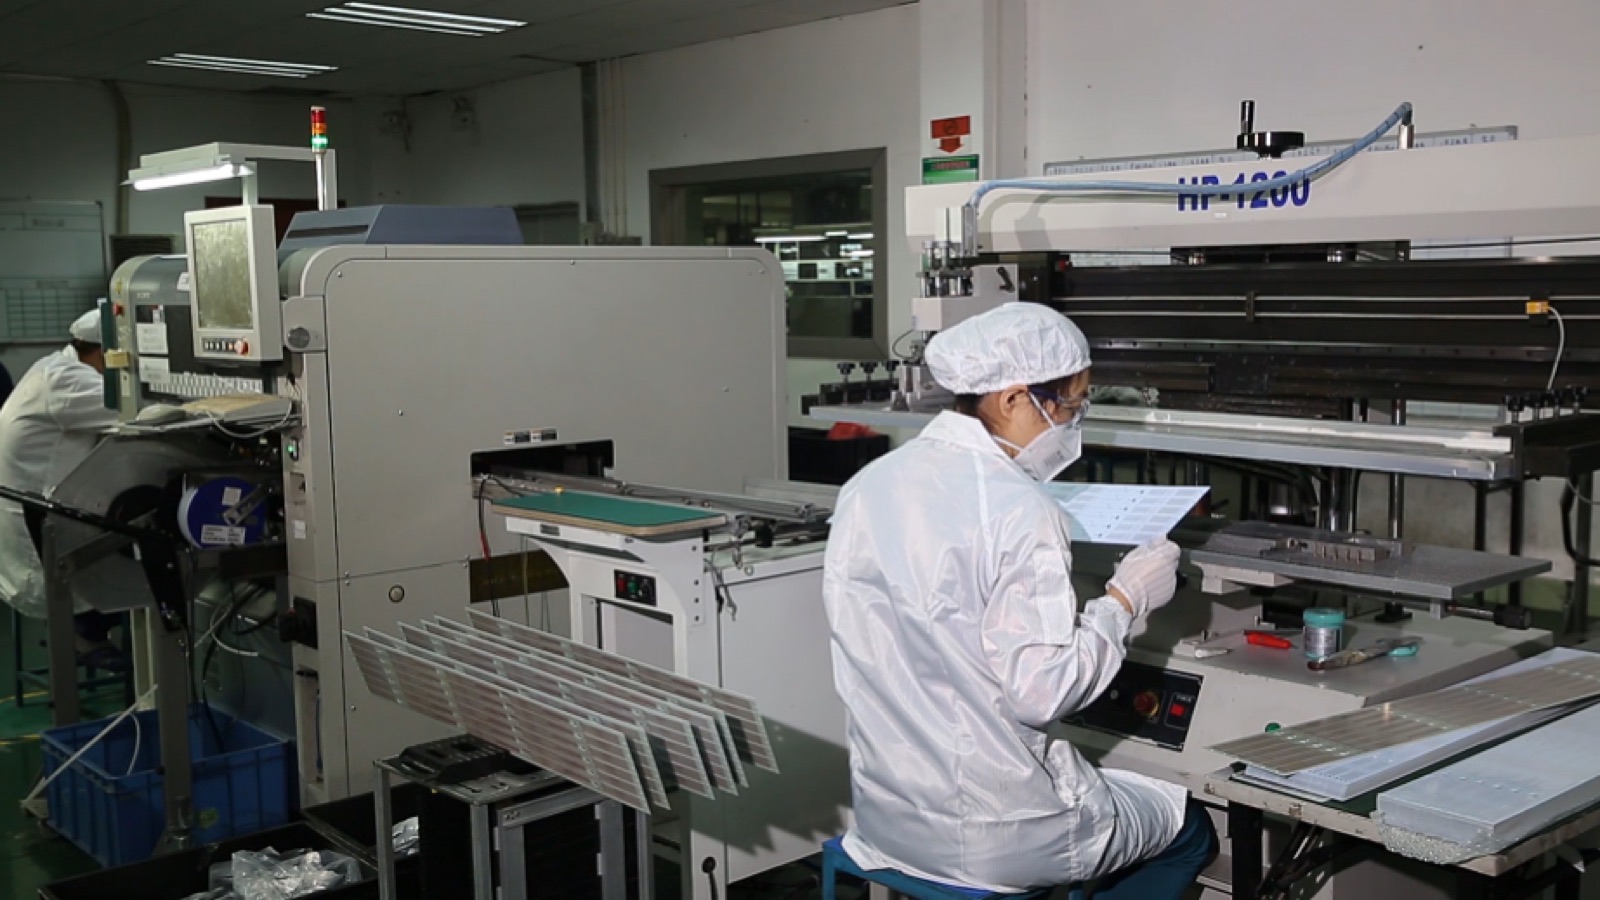
Our SMT shop places and solders the LED boards and driver components, and it is the most automatable — therefore most controllable — part of the chain. Solder-paste inspection happens before reflow; post-reflow inspection catches bridging and misalignment; electrical testing catches what eyes cannot. Per-shift IPQC sampling tracks the trend lines, because process drift announces itself in statistics before it announces itself in failures.
Why does this matter to a buyer choosing between factories? Because LED fixture reliability is dominated by solder joints and thermal management, both of which are made or broken at SMT and neither of which shows in a product photo. When you audit a factory, stand at the SMT inspection station for ten minutes and watch what gets rejected. That ten minutes tells you more than the certificate folder in the meeting room.
Aging, safety and the tests behind 'it works'
Final inspection is not just 'does it light'. Every sampled unit runs functional aging — hours of operation that flush out early-life failures (what reliability engineers call infant mortality). Safety testing includes high-potential (dielectric strength) checks between live parts and accessible metal, earth-continuity checks on Class I fittings, and thermal checks on driver compartments. None of this is exotic; all of it is skipped somewhere, and the skipping shows up as field failures in year one rather than year five.
The standards we engineer to depend on the destination market — UL, VDE/TÜV, PSE, SAA expectations — and the group's manufacturing operations are certified to ISO 9001, 14001, 45001 and 50001. Certification of the factory and certification of the product are different things, by the way; a factory can hold ISO and still ship a product that has never seen a test lab. Ask for both, per model.
AQL sampling in plain numbers
Final inspection follows AQL (Acceptable Quality Limit) sampling — the ISO 2859 method that decides how many units to inspect per batch and what defect count passes. The arithmetic surprises people, so here is a real example at the common general-goods level, AQL 2.5:
| Batch size | Sample inspected | Accept if defects ≤ | Reject if defects ≥ |
|---|---|---|---|
| 91–150 units | 20 | 0 | 1 |
| 151–280 units | 32 | 1 | 2 |
| 281–500 units | 50 | 2 | 3 |
| 501–1,200 units | 80 | 4 | 5 |
| 1,201–3,200 units | 125 | 6 | 7 |
Golden sample discipline
Before mass production, an approved golden sample is signed by both sides — for custom work it carries your finish, packaging and markings. Every production unit is judged against it. This single artefact resolves most of what otherwise becomes argument: is this colour 'close enough'? Does the beam match? The golden sample answers, physically, what a specification can only approximate in words.
It also anchors repeat orders. Your third PO ships against the same golden sample as your first, and our IQC verifies incoming bins against it — not just against a datasheet. For ODM projects the golden sample plus the signed specification form the complete reference; if a discrepancy is ever disputed, both sides go look at the same object rather than at each other's interpretation.
Third-party inspection: how we cooperate
We encourage buyer-appointed or third-party inspection — SGS, TÜV, Bureau Veritas or your own agent — and treat inspectors as guests with access, not adversaries. We provide the golden sample, the AQL plan and a sampling location in advance so the inspection day is spent inspecting rather than negotiating scope. Inspectors who find a real defect are doing our quality system a favour; the cost of a caught defect is trivial next to the cost of a shipped one.
A buyer-side tip: book third-party inspection after pre-shipment packing has started, so the inspector samples packed cartons against the packing list — the fourth gate — rather than loose units. And send the inspector the golden sample reference in writing; it is the one instruction that prevents most ambiguous reports.
What to take from this
Four gates, honest sampling arithmetic, a golden sample both sides have touched, and traceability that survives past the shipment. That is the whole system — everything else is paperwork around it. If you are evaluating factories, ask each one to walk you through their gates in this much detail; the ones who can, and the ones who pivot to certificate photos, sort themselves quickly. If you would rather see it directly: factory visits are welcome for qualified partners, and the SMT inspection station is on the tour.
Quick answers
Can we appoint a third-party inspection before shipment?
Yes, and we encourage it. We cooperate with buyer-appointed inspectors (SGS, TÜV, Bureau Veritas or your own agent) and provide the golden sample and AQL plan as the inspection basis.
What AQL do you work to?
Standard general goods AQL 2.5 / 4.0 unless your agreement specifies stricter levels. Hotel and project programmes often run AQL 1.0 — we quote to your requirement and record it as the inspection basis.
Do you age-test finished fixtures?
Yes — final inspection includes functional aging per product family, which flushes out early-life failures before shipment. Duration and conditions are documented in the test standard we can share per model.
How are LED colour bins controlled across repeat orders?
Chips are procured to specified bins (3-step SDCM or better for project orders) and verified at IQC against the golden sample, so repeat orders match your first order — not just the datasheet.
What happens if a final inspection finds defects?
Defective units are repaired or scrapped and the batch is re-audited with a tighter acceptance level. The line does not resume until the deviation is corrected and recorded at IPQC.
Can we visit the factory before ordering?
Yes — factory visits are welcome for qualified partners, including the SMT line and spray shop. Contact us with your company details and intended programme to arrange it.